If you work in a structural steel fabrication shop, this probably sounds familiar: the model is done in Tekla, the order is in the ERP, and yet nobody on the shop floor can tell you where a given beam is right now, which heat it was cut from, or who welded it against which WPS. That information lives on paper, in spreadsheets and in chat groups. A manufacturing execution system exists to close exactly that gap.
What is MES? The short definition
A Manufacturing Execution System (MES) records and controls the execution of production on the shop floor: which operation, on which part, with which material, by whom, when, and with what result. If the ERP says what should be built and what it costs, the MES says what is actually being built right now and what state it is in.
The reference standard is ISA-95, which describes a plant in layers: level 4 is business planning (ERP), level 3 is manufacturing operations management (where MES sits), and the levels below are machine and line control. MES is the bridge between the office and the floor. ISA's own summary describes level 3 as MES and systems such as SCADA that manage manufacturing operations, and says the standard deals mainly with the interface between levels 3 and 4, which is the hand-over between MES and ERP.
What does a manufacturing execution system actually do?
The classic MESA model lists eleven functions. For a steel fabricator, these are the ones that matter most:
- Product tracking and genealogy: every part is linked to its parent plate or section, its heat number and the mill test certificate (MTC).
- Dispatching: which parts go to cutting, drilling, welding or painting today.
- Shop-floor data collection: start and finish of each operation captured when it happens, not written from memory at the end of the shift.
- Quality management: inspections, NDT results, non-conformance reports (NCR) and corrective actions, all attached to the same part.
- Document control: welders work from the current WPS and drawing revision, not last month's.
- Performance analysis: progress reported from finished parts and tonnage, not estimates.
Why MES looks different in steel fabrication
Most "what is MES" articles assume high-volume, repetitive production. Structural steel isn't like that. A project has thousands of one-off parts, drawings change mid-job, and the client or inspector expects a full history for every beam and column. That shifts the priorities:
- Data comes from the model, not from typing. If someone has to re-key the part list from Tekla, errors are built in from day one.
- Heat-to-part traceability. When a material certificate is questioned, you need to know within minutes which parts came from that plate and where they are now. The same heat-to-part records are what a digital product passport for steel will be built on.
- Weld quality and records. WPS, welder qualification (WPQ) and NDT results must be tied to the part, so the manufacturing record book (MRB) at handover is generated, not assembled by hand.
- Working without internet. Large fabrication halls often have poor Wi-Fi. A system that stops when the network drops gets abandoned.
A real example: SteelFlow MES
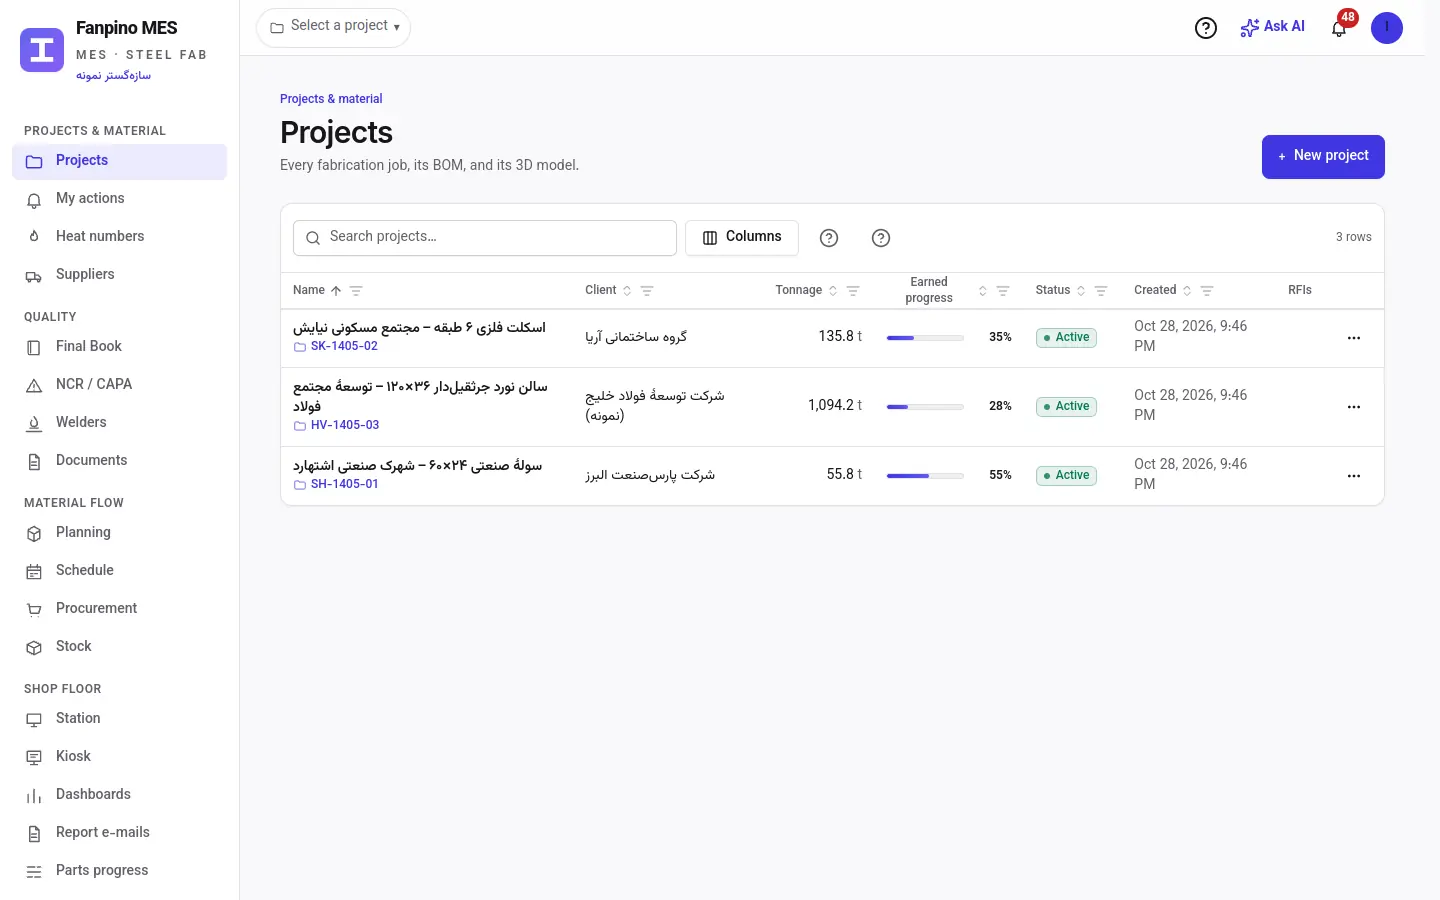
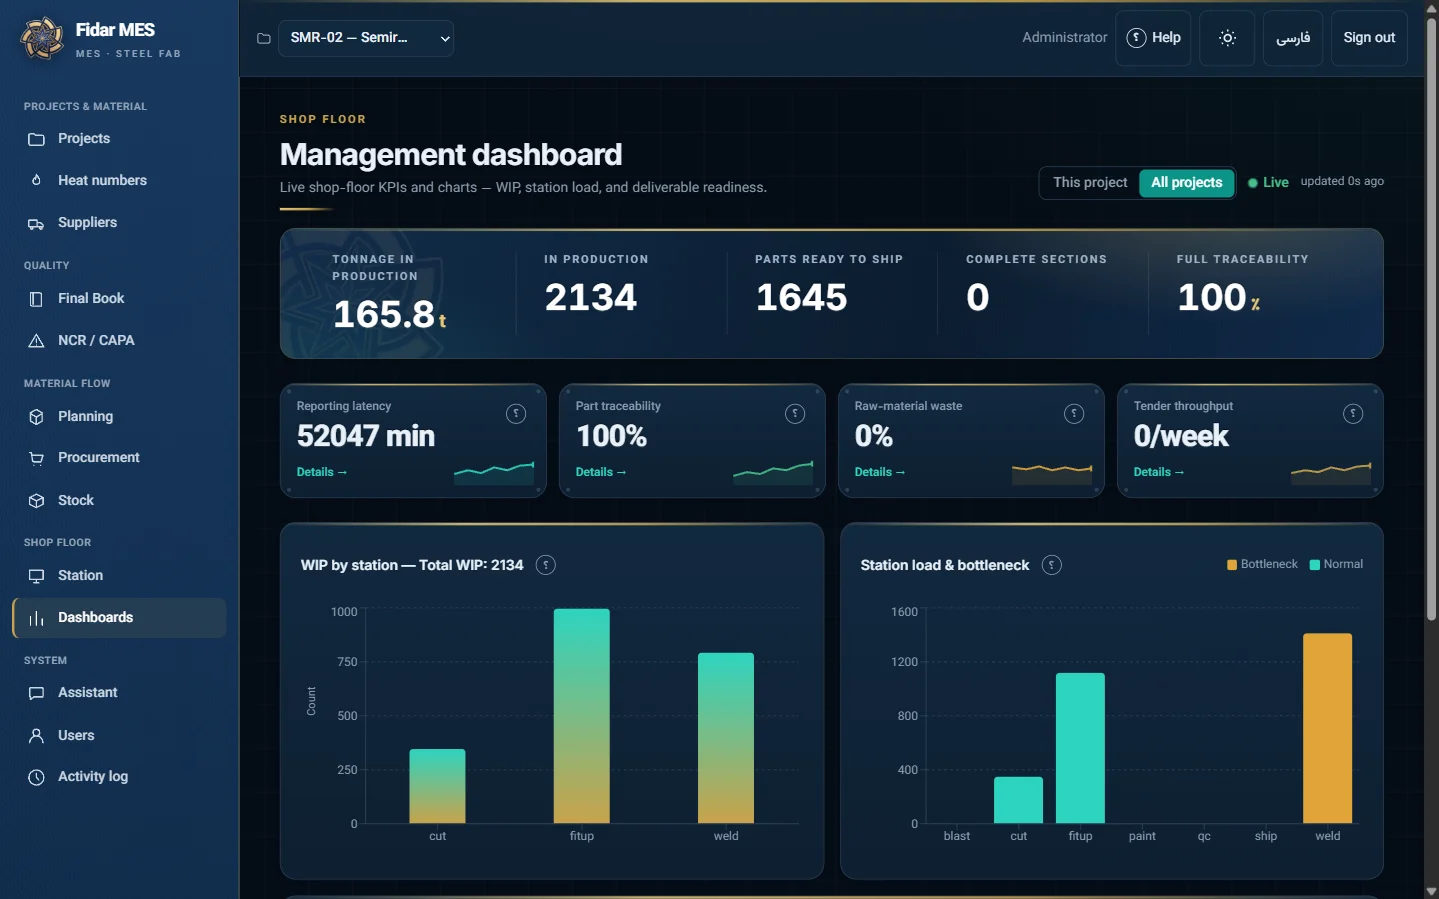
At Fanpino we built an MES specifically for structural steel fabrication, called SteelFlow. Following one part through it makes the definitions concrete:
- Tekla to BOM: the model comes in through a Tekla plugin and the bill of materials is generated automatically. Importing the same model twice creates no duplicate; a changed model creates a new version. Details in Tekla to BOM without manual re-entry.
- Heat → material → part: for any part you can see which material and which heat number it came from.
- The shop floor, even offline: the floor app runs on tablets, keeps working when the connection drops and syncs later. We tested it in airplane mode. Why that matters: offline shop floor vs cloud MES.
- Quality linked to the part: WPS/WPQ, NDT, coating, NCR and corrective action are all attached to the part, and the MRB is built from that data. More in this article.
- Dashboards, planning and procurement: progress KPIs, production planning, nesting and material purchasing live in the same system, not a separate spreadsheet.
MES vs ERP in one paragraph
ERP is about money, orders, inventory and accounting, and usually works at the level of days or weeks. MES is about production itself, at the level of minutes and individual parts. They are not competitors: ideally the ERP hands orders to the MES, and the MES reports actual material use and progress back. For which one a steel fabricator needs first, see MES vs ERP for steel fabrication.
MES implementation, step by step
A rollout that sticks usually follows the same order, with each stage settled before the next one starts:
- Scope one product flow. Pick the parts and stations that cause the most chasing today, for example cut, fit and weld on one bay, and write down what has to be traceable at each one.
- Build the data spine. Model import, BOM, routings and the link from heat number to material to part. Everything later depends on this being right.
- Run a pilot line. One bay or one project, real parts, real operators. Fix whatever makes logging slower than paper before going further.
- Add barcode or QR stations. A scan at each station replaces end-of-shift notes; the floor app has to keep working offline.
- Connect quality. Attach WPS, NDT results, coating checks and NCRs to the same part records.
- Link the ERP. Orders come in from the ERP, actual material use and progress go back. No second accounting system.
- Roll out in stages. Extend bay by bay, then add dashboards and planning once the data behind them is flowing on its own.
Core MES modules
- Product tracking and genealogy
- Dispatching and work orders
- Shop-floor data collection
- Quality management (inspection, NDT, NCR)
- Document control (drawings, WPS)
- Performance analysis and dashboards
Common mistakes when rolling out MES software
- Starting with dashboards. A dashboard fed by manual entry is empty within two months. Get data flowing automatically from the source first.
- More work for operators. If logging an operation is harder than writing it on paper, paper wins. Floor screens have to work on a tablet, with gloves, in the local language.
- Rebuilding the ERP. The MES doesn't need its own accounting or inventory; it needs to exchange data with the ERP you have.
- Ignoring network outages. The first outage that stops the floor is the last day people trust the system.
- Big-bang go-live. Roll out in stages and let each one settle before the next.
Comparing tools? See SteelFlow MES vs Tekla PowerFab: where each one fits.
FAQ
Is MES only for large plants?
No. Mid-sized, project-based shops that care about traceability and quality records benefit too, as long as the system starts simple and doesn't add work on the floor.
On-premise or cloud?
Both work. When project data is sensitive or the internet is unreliable, on-premise makes more sense. What matters more than where it runs is that the floor keeps working offline. If your shop also works around scheduled grid cuts, see planning a steel fabrication shop around power cuts.
How long does an MES rollout take?
It depends on scope. Start with the data spine (model import, BOM, traceability), then add the shop floor and quality. Trying to launch everything at once is the most common way these projects stall.
Where does AI fit?
AI only helps once clean, connected data exists. In SteelFlow the AI assistant came last and is read-only. Data first, AI after.
What does MES stand for?
Manufacturing Execution System: software that records and controls production on the shop floor, meaning which operation ran on which part, with which material, by whom, when and with what result. ERP plans and costs the work; MES tracks it as it happens.
Where does MES sit in ISA-95?
At level 3, manufacturing operations management. ERP sits at level 4, business planning and logistics, and ISA says the standard deals mainly with the interface between those two levels.
What is different about MES for steel fabrication?
Steel fabrication is project-based with thousands of one-off parts, so the MES has to take its part list from the Tekla model, trace every part to its heat number, tie welds to WPS, welder and NDT results so the MRB is generated, and keep working when the hall loses its network.